Showing posts with label DRINKING WATER. Show all posts

JANICKI BIOENERGY


"The project is called the Omniprocessor, and it was designed and built by Janicki Bioenergy, an engineering firm based north of Seattle. I recently went to Janicki’s headquarters to check out an Omniprocessor before the start of a pilot project in Senegal.

The Omniprocessor is a safe repository for human waste. Today, in many places without modern sewage systems, truckers take the waste from latrines and dump it into the nearest river or the ocean—or at a treatment facility that doesn’t actually treat the sewage. Either way, it often ends up in the water supply. If they took it to the Omniprocessor instead, it would be burned safely. The machine runs at such a high temperature (1000 degrees Celsius) that there’s no nasty smell; in fact it meets all the emissions standards set by the U.S. government.

Before we even started the tour, I had a question: Don’t modern sewage plants already incinerate waste? I learned that some just turn the waste into solids that are stored in the desert. Others burn it using diesel or some other fuel that they buy. That means they use a lot of energy, which makes them impractical in most poor countries.

The Omniprocessor solves that problem. Through the ingenious use of a steam engine, it produces more than enough energy to burn the next batch of waste. In other words, it powers itself, with electricity to spare. The next-generation processor, more advanced than the one I saw, will handle waste from 100,000 people, producing up to 86,000 liters of potable water a day and a net 250 kw of electricity."


How much does it cost?
"Around $1.5 million, but I would not focus too much on that. This machine is a great profit center compared with many waste-processing systems we have. They'll recover it very fast."


My thoughts...
I have a feeling that the Omniprocessor which uses a steam engine is based on the Sterling engine which Dean Kamen has been working on for the last 15-20 years.

Dean Kamen has a water purification system called the Slingshot.

Janicki's "parent company" is a full fledged engineering company too.


  1. http://www.gatesnotes.com/About-Bill-Gates/A-Day-at-DEKA-Research-with-Dean-Kamen
  2. http://www.forbes.com/sites/christopherhelman/2014/07/02/dean-kamen-thinks-his-new-stirling-engine-could-power-the-world/
  3. http://www.wired.com/2015/01/omniprocessor/

POLYMEM


  • Polymem is an independent company located in the “membrane technology valley” of Toulouse –France. It has been founded in 1997 by two engineers having more than 25 years experience in Hollow Fiber Membrane manufacturing for water treatment purposes
  • Polymem is continuously improving his products and processes and is so involved in major national and European research projects in the membrane field. For its innovation policy, Polymem has received the « 2000 Innovation Award » from the INPI (French National Institute for Intellectual Property)
  • Polymem is developing strong partnerships in the world for supporting the OEM companies that are choosing Polymem products in their respective markets and countries
  • Module range NSF/ANSI 61 approved (American Public Health and Security Company) and ACS approved (French Ministry of Health)
  • More than 250 installations worldwide


Polymem manufactures turnkey filtration systems.

We offer standard Aquamem ™ systems or custom made systems.

Aquamem® UF100L/LL: units from 0.5 to 5 m3/h
The range Aquamem® UF100L (UF100L AQM) is composed of compact and modular ultrafiltration units, easy to install and use. Economical with low maintenance, these compact and lightweight units allow the production from 500 l / h to 5 m3 / h.
Two sets of units are composing the range: manual AQM UF100L and Automatic AQM-UF100L.

Aquamem® UF80: Units from 5 to 20 m3/h
These standard skids, compact and autonomous are delivered ready to be connected electrically and hydraulically.

Aquamem® UF120: Units from 20 to 100 m3/h
These standard skids, compact and autonomous are delivered ready to be connected electrically and hydraulically.
Racks with Ultramem and Gigamem® module: from 100 m3/h capacity

Aquamem® mobile: units easily transportable.
For any application that requires a containerized unit (mobile unit for emergency use or installation without appropriate infrastructure), Polymem offers standard or custom made solutions.


LIFEWATER ENGINEERING COMPANY


Lifewater Engineering Company has been building packaged water and wastewater treatment systems in Alaska, USA for the past 15 years. Experts in arctic design (-60°F/-51°C) and solutions for utility construction on permafrost and difficult soils,  Lifewater designs and builds systems ranging in size from large man camps and hotels to a single family residence. Lifewater has extensive experience with remote applications where reliability is critical and transportation of packaged plants is limiting.


Lifewater uses membrane bioreactor (MBR) technology as well as various fixed film processes for wastewater treatment depending on project requirements. Lifewater systems are compact and can be controlled and monitored remotely. 


ExtremeSTP™ Sewage Treatment Plant Containerized MBRs;

Commercial ExtremeSTP™ sewage treatment plants are designed for use anywhere on Earth, including extremely cold climates (-60oF/-51oC). Each system can be customized to meet the client’s needs. Our typical membrane bioreactor (MBR) treatment process includes a surge tank, a fine solids removing screen, bioreactor to provided aerobic decomposition, tubular membrane ultrafiltration, UV disinfection, and dosed effluent discharge.


PURE H2O


Pure H2O are a Danish-owned company who produce and market mobile water purifiers for use in areas affected by natural disasters or other places where clean drinking water is scarce.

Pure H2O produces mobile and modular clean drinking water solutions through its water purification concept called the BlueBox concept.

The concept is based on reverse osmosis filtration technology, and consists of cartridge filters, active carbon and UV light. The purification method is well known and used widely.

Superior water filtration systems

All Pure H2O's water systems are made with the finest grade stainless steel and other non-corrosive materials - we only use the best.

Our system is fitted with proven superior membranes. The reverse osmosis filtration process relies on a very dense membrane through which only water and some low-molecular weight compounds pass.

This means that the feed stream is divided into a permeate containing pure water and the concentrate which contains all dissolved solids.

Water filtration systems for the defence industry

The BlueBox concept has been sold in many countries and to military and emergency deployment organisations as well as armed forces authorities.
They choose the BlueBox concept because of its 'best-in-class' features such as our filtration design mixed with high modularity. We can provide clean water solutions from 450l/hr up to 4,000l/hr.
Our standard solutions are designed to comply with basic needs and typical client criteria. We always listen to your special needs in order to accommodate a solution that is the most useful for you. Here is a short listing of basic criteria met by the BlueBox concept:
  • Energy efficiency and low running costs: you pay only for what you need, and at a low production cost, making this machine very cost efficient on the long term. Let us assist you in calculating costs
  • Durability for years: with the right maintenance, this machine will endure many years of providing drinking water. You have solved any drinking water issue for a very long time, and can focus your efforts on other important activities
  • Drinking quality and health standards compliance: through state of the art components and reverse osmosis technology you can always be sure that the BlueBox concept will produce the best drinking water quality, and have security in the knowledge that we comply with the World Health Organisation's (WHO) quality standards. Water purified through Pure H2O's BlueBox plant has been tested at state-controlled Danish and foreign laboratories. The tests demonstrate that end users at virtually all places with access to surface water can get clean drinking water that is in compliance with WHO standards
  • Environment friendly solutions: the units do not contain oil or chemicals that may adversely impact the environment. Add our solar array and you are free of the need for fossil fuels
A combination of filtering methods, sturdy material, simple construction in a plastic container, easy operation, large capacity, low energy consumption and mobility is what makes Pure H2O products unique.

BlueBox 4000

The BlueBox 4000 is a mobile water purification unit in 2 cubic boxes.

Fast Response Time: Operative shortly after reaching deployment site
Easy, Simple: Anyone can operate the units with a minimum of training
Mobilility: 1.2 by 1.2 meters and stacked 2 by 2, they fit snugly into standard 20ft and 40ft containers
Health: Supplies safe water for drinking, cooking, bathing, cleaning, laundry;
- keeping men on their feet
Capacity: 1 unit produces 90 m3/day
The purification machines are simple to operate; the control system basically consists of Start/Stop buttons and a few manometers to keep track of working pressure and production.

SELDON TECHNOLOGIES INC


Seldon Technologies’ mission is to fully explore, develop, perfect and apply the amazing material properties of the carbon nanotube: large surface area, great strength, light weight, high electrical conductivity, and rapid heat transport.


We solve customer (end-user) problems in fluid filtration, purification, and separation using Nanomesh™, breakthrough and patented carbon nanotube (CNT) composite technology. Nanomesh turns unhealthy water into purified, great-tasting drinking water. We have designed a product line using this technology that combines ease of use with dependability and safety.

At Seldon, we have taken nanomesh from the lab into the field. Our team has created a group of products that remove 99.9999 percent of the bacteria in water; 99.99 percent of the viruses; and 99.9 percent of the cysts. They provide the preferred, point-of-use drinking water technology for a wide variety of applications, including military, disaster relief, and consumer markets.These products are easy to use, patent-protected (U.S. 7,211,320; U.S. 7,419,601; U.S. 7,682,654, and U.S. 7,815,806) and standards-based.

WaterBox™ 300 MIL

The Seldon Waterbox™ 300 MIL delivers pure water in less than five minutes.

Built with Seldon’s Nanomesh™ Technology, the WaterBox 300 MIL absorbs contaminants from groundwater and produces drinking water that meets the USEPA Drinking Water Standard. Bacteria, viruses, cysts, spores and other contaminants are immediately eliminated without the need for heat, ultra-violet light, chemicals, or electricity.

A simple plug-and-use system, the WaterBox is easy to use. Immediate, high quality results set the WaterBox apart from all other purification systems.


Features


  • Removes bacteria, viruses, Cryptosporidium, and Giardia to USEPA drinking water standards: 99.9999% of bacteria, 99.99% of viruses, and 99.9% of cysts
  • Exceeds USEPA drinking water standard
  • Reduces sediments, chlorine, total organic carbons, bad taste, and odors
  • Reduces chemicals and many harmful heavy metals (e.g., mercury and lead)
  • Self-priming system can pump from any water source with up to 4.3 meters (14 feet) of lift
  • Simple, flow-through design
  • Electrical components adaptable to any field situation: 12VDC internal operating components (pump) allow for any electrical conversion either to 12VDC, 24VDC, 115VAC 60 Hz, or 230VAC 50 Hz
  • Lightweight and rugged casing and components
  • Patented Nanomesh technology for high-performance contaminant removal
  • One-year warranty

Specifications


  • Capacity: up to 30,000 liters (8,000 gallons), depending on water quality
  • Flow rate: 1.89 liters (0.5 gallons) per minute
  • Inlet water: system is self-priming and can pump from any water source with up to 4.3 meters (14 feet) of lift
  • Dimensions: 24.9” length × 23.7” width × 13.1” height (632 mm × 602 mm × 290 mm)
  • Weight: 78 pounds (31.8 kg)
  • Power source: 12VDC, 24VDC, 115VAC 60-Hz, or 230VAC 50-Hz

SLINGSHOT - DEKA RESEARCH AND DEVELOPMENT


The undistinguished looking box stands about waist high, weighs less than 300 lbs and has all the charm of a motel icemaker. But its potential is much greater. It just might be the greatest packaged water treatment plant ever.
The box may become the unsung revolutionary tool that transforms life for great numbers of the world’s population. It is called Slingshot, a vapor compression water purification machine produced by genius inventor Dean Kamen, the man best known as creator of the Segway transporter. Slingshot can produce roughly 30 liters of water an hour using no more energy than required by a standard handheld hair dryer.


Kamen has been developing this technology for more than a decade. The name Slingshot refers to a weapon for defeating a Goliath of a problem. He showed it off on 60 Minutes in 2003. In 2008 he appeared on The Colbert Report, operating a Slingshot on the air and drinking its product.
But this fall, Kamen began the process that may at last get Slingshot machines into the remote villages of the world where it is most needed.


The Slingshot system of vapor compression distillation basically boils and then condenses any dirty water source. It is versatile and can use energy from many sources — a standard electric grid, solar cells, batteries, or even methane from animal dung.


Coca-Cola and DEKA R&D will partner with IDB and the Multilateral Investment Fund (MIF), a member of IDB Group, to initially test the Slingshot technology in health centers and schools in remote communities in Latin America in 2013.


BLUMETRIC ENVIRONMENTAL INC (SEPROTECH)

Seprotech Systems Incorporated (TSX-V: SET; “Seprotech” or the “Company”) is pleased to advise that at the Company’s special meeting of shareholders held on October 24, 2012, the shareholders approved, subject to the final approval of the TSX Venture Exchange (“TSX.V”), the proposed acquisition of WESA Group Inc. (“WESA”).  The resolution was approved by a majority of the votes cast by shareholders, excluding the votes cast by any shareholders required to be excluded from voting.

The shareholders also approved the following:
  1. The change of name of the Company to “BluMetric Environmental Inc.”
  2. The consolidation of the common shares of the Company on a 1-for-10 basis
  3. The reduction in stated capital of the Company to $1
  4. An amendment to the Share Option Plan of the Company increasing the number of shares that may be issued thereunder to 3,200,000 (after giving effect to the share consolidation). Certain Insiders and their affiliates were excluded from voting on the amendment.
Pursuant to the share exchange agreement, Seprotech will acquire 100% of privately held WESA in a reverse takeover (the “Transaction”). Upon completion of the Transaction, the combined entity (the “Resulting Issuer”) is expected to be a leading provider of earth science and environmental engineering services, and wastewater and water treatment systems. The intent is to build an integrated product and service organization that provides intelligent solutions to complex environmental problems both in Canada and abroad.


The CLEMENTINE® is a wastewater plant in a standard 20’ ISO container. Designed
for transport by land, sea and air, this extremely versatile machine is purpose built to
be transported just about anywhere under just about any conditions. There are no
exterior tanks, holding ponds or exterior components. Quiet and free of unpleasant
odours, this is the perfect wastewater solution for hard to get to remote sites and
temporary camps or installations.

CLEMENTINE® is a complete wastewater treatment plant in a box. Everything needed
to treat wastewater is in the single unit. This plant is a plug and play system that is very
easy to operate and maintain. If you can operate a portable generator then you can
operate a CLEMENTINE®. See specifications on reverse.


Some ideal applications for the CLEMENTINE® are:
  • Mining camps
  • Military camps
  • Construction camps
  • Oil rigs and pipelines
  • Areas accessible only by air
  • Environmental emergencies
  • Foreign relief missions
  • Temporary municipal services

HYDROSECURE


HydroSecure® was initially developed to protect senior government executives and mission critical facilities, such as embassies, operations centers, and executive residences. After the terrorist attacks of September 11, 2001, the Department of Defense, the State Department, and the United States Secret Service collaborated to seek the best available system for water security. HydroSecure was selected through a competitive solicitation and thoroughly tested in government laboratories.
 

HydroSecure® demonstrated superior performance and effectiveness in a series of tests purifying water that was highly contaminated with a variety of biological and chemical agents designed to simulate the “maximum credible threat scenario”. The tested contaminants included biological and chemical warfare agents, industrial and agricultural chemicals, biological toxins, and hallucinogenic drugs. HydroSecure was also tested for reliability of performance and long-term sustainability in harsh operating conditions.

 
The government has allowed us to make this system available to the commercial market and it is now available for the first time in a new, compact design. This new patent-pending, design, the HydroSecure II® series, is your opportunity to have the same approach to post-9/11 drinking water security that the U.S. government selected to safeguard high profile individuals & installations throughout the U.S.
 

 SPECIFICATIONS
• Up to 8800 GPD production
• 165 gallon water storage tank included, larger storage optional
• Connects to standard size 3/4” water line or larger
• Standard 240 VAC power
• Dimensions: 32”wide X 27”deep X 65”high (0.8m X 0.68m X 1.6m)

OPTIONAL FEATURES
• Integrated touch screen controls
• Remote monitoring and management
• Continuous data logging and trend analysis
• Integration with household security systems


• Water that is free of objectionable chemicals such as chlorine, chloramines and possible
other disinfection by-products (DBP’s)
• Water that is free of hard-water limestone deposits without the need to add the
chemicals typical of traditional water softening
• Water that reduces costly maintenance of equipment and appliances normally associated
with hard water
• Water for bathing that is crystal clear, soft and free of chemicals
• Drinking water for you and your loved ones that you know is more pure and safer than
bottled water.
• “Plug-and-Play” operation, with all components pre-assembled in one unit for easy,
quick installation
• A five‐stage purification process for maximum effectiveness
• A sleek aluminum frame that fits in new or existing structures where access/space may
be limited
• Whisper‐quiet operation


MANN+HUMMEL WATER FILTRATION


MANN+HUMMEL established its Water Filtration Division to provide better services to worldwide clientele answering the needs for reliable and cost effective clean water systems. Globally headquartered in Singapore, MANN+HUMMEL Water Filtration Division provides clean water solutions around the globe, delivering safe, clean water for a variety of commercial and industrial use. With our extensive expertise and range of affordable systems, we realize clean and pure water for rural communities, manufacturers and industrial operations. As a water and wastewater treatment provider to global clients, MANN+HUMMEL design and manufacture our own modular systems with high quality membranes.

MemBio Series (Membrane Bioreactor) - Offering a one-step process for water recycling through the removal of suspended solids and micro-organisms, our Membrane Bio-Reactor Systems help achieves 50% space savings with its economical operation footprint. Through the use of hollow fibre membrane technology, the Membrane Bio-Reactor System may be applied for treatment of sewage effluents and other waste streams with high COD or BOD.


Klar Series (Ultrafiltration) - Able to provide a safe and consistent water supply without the use of water purification chemicals, our Ultrafiltration Systems offer substantial cost savings and low logistical and operational requirements.

Our systems are capable of removing foreign particles, bacteria, spores and parasites. They attain a turbidity of less than 0.1 NTU, and have a high bacteria removal rate. The Ultrafiltration system is suitable for clarification of wastewater, river, well and surface water, as well as colloidal suspended solids separation.


NEWTERRA


newterra is a global technology leader in the development of sustainable solutions for the treatment of wastewater, greywater and process water, as well as groundwater remediation, for industrial and municipal markets. In operation since 1992, newterra’s customers include Fortune 500 resource companies, major engineering consultants, industry, agriculture and food businesses, and small- to medium-sized municipalities.

newterra engineers, designs, manufactures and supports its innovative treatment systems, some of which operate in extreme conditions in the most remote areas on the planet. The collaboration of newterra’s research & development, design and manufacturing teams has allowed the company to pioneer our innovative MicroClear™ Membrane Bioreactor (MBR) technology, sound attenuated remediation systems for use in residential areas, and iron removal processes for groundwater treatment.

newterra is at the forefront of MBR technology and its use in a wide range of wastewater treatment applications. Membrane Bioreactors combine conventional activated sludge (CAS) treatment with a membrane liquid-solid separation process. Our MBR products are treating sewage to near-potable quality in thousands of systems worldwide. These include remote work camps for resource industries, decentralized systems for municipalities, resorts, and industrial and agricultural applications.

The core of newterra MBR wastewater treatment systems is our patented MicroClear membrane. These units are submerged directly into the wastewater and filtrate (filtered water) is drawn through and out of the membrane by a slight negative pressure. Solids, bacteria, parasites and viruses remain in the bioreactor to be digested by bacteria or settle as sludge. newterra MBRs eliminate the need for the final stages of conventional wastewater treatment plants, including clarification and filtration.

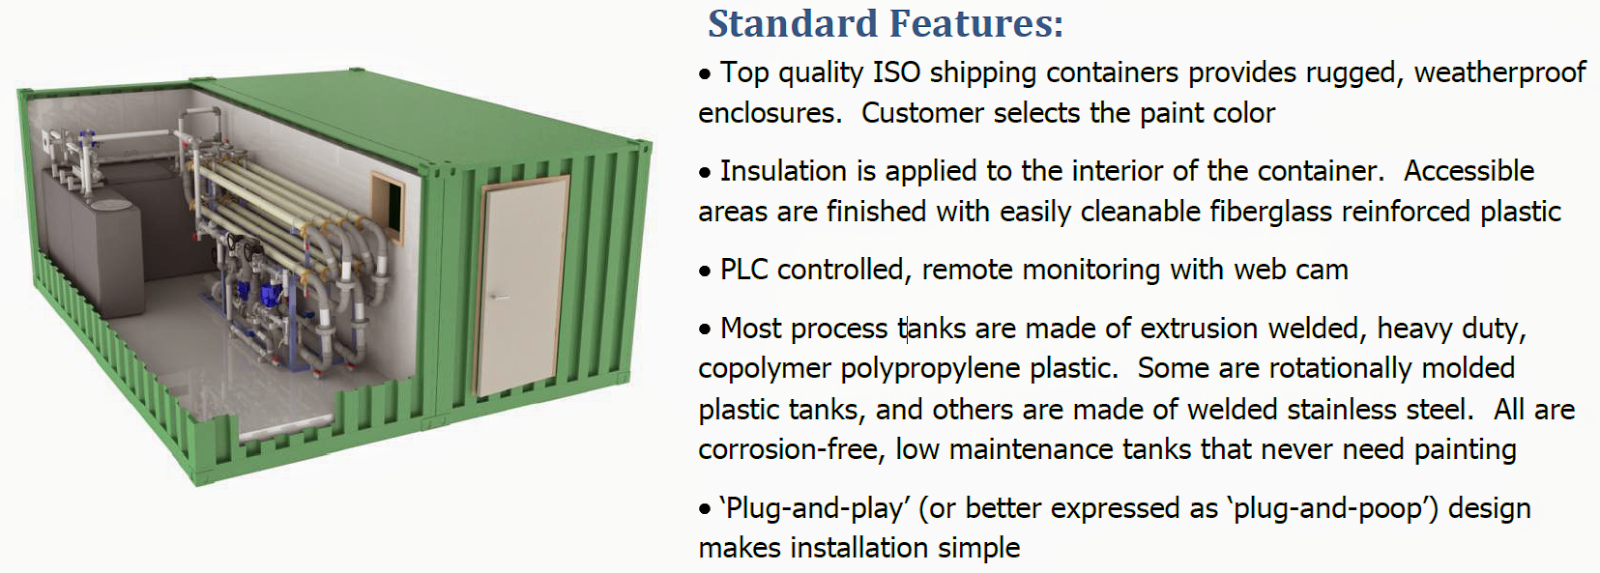
At newterra, our depth of experience in water-related solutions includes the provision of potable water systems. Our engineering team will integrate the filtration, storage, pumping, flow measurement, disinfection, electrical, and instrumentation and control/telemetry systems to meet your specific requirements. Our systems can be skid mounted or configured into a enclosure.
newterra potable water systems employ safe, proven treatment technologies including conventional and membrane filtration and ultraviolet disinfection – all designed to meet stringent drinking water quality standards. Talk to us about your water needs.

SECCUA


Seccua is a global technology leader in the field of standardized, packaged ultrafiltration
systems for process and drinking water. Bacteria, viruses, Legionella and parasites;
turbidity, colloids and coloration due to iron can be effectively removed from drinking water
without the addition of chemicals.

More than10 years of experience in the field of ultrafiltration have culminated in systems
with proprietary control systems incorporating automatic membrane integrity testing, data
logging and remote monitoring and control. Our certified module manufacturing enables us
to offer custom sized UF modules to OEM’s, and our system manufacturing is capable of
producing over 1,500 systems annually.


 Based in Steingaden, near Munich, Germany, and Surprise, Arizona, Seccua has installed
over 400 ultrafiltration systems for residential, commercial and small-systems municipal
applications. Products from Seccua are primarily aimed at local water supplies and
industrial water treatment.


These compact systems can filter up to 30,000 liters of water an
hour (132 GPM), and are easy and inexpensive to install and operate. They are fully
automated and require low maintenance. They are ideal for places and areas not connected
to central water supplies, but are also widely applied in industrial treatment processes that
need full removal of pathogens and suspended solids.


The flagship in Seccua's product range is the Virex Pro system. This intelligent filtration
system can purify up to a maximum of 3,900 litres of water an hour (18 GPM). It
automatically detects how badly contaminated the filter is and automatically carries out
cleaning processes at the appropriate intervals, if required with automated chemical
enhancement. The control unit independently adjusts the interval between filter cleans, as
well as the length of each filter clean, depending on the water quality, thereby ensuring
simple operation and optimized running costs. The Virex Pro and Phoenix systems also
feature an integrated membrane integrity test:


The membrane filters used are regularly and independently checked for damage. In the
event of a membrane fault, the system is stopped automatically and triggers an alarm locally
and remotely. Thanks to this innovation, the removal of pathogenic organisms from the
drinking water and a constant high quality of water can be assured. Seccua is the world
market leader for this patented technology.


ASPEN WATER PRODUCTS


Aspen Water purification systems produce more water with less power than any other portable water purification system on the planet.  Water can be drawn from virtually any water source including sea water, ditches, ponds, rivers, lakes, swimming pools or standing water that may contain chemical and biological contamination.


Aspen Water systems are made in the USA, and its corporate headquarters are located in Richardson, Texas.

Aspen Water Products are available thru GSA Advantage, used by the U.S. Military and disaster relief organizations around the world, and have proven themselves under some of the most demanding an extreme conditions, including field testing at the Aberdeen Proving Grounds.

Types of Systems
  • The Aspen 2000DM is the most compact, versatile, full featured, computer controlled, energy efficient, mobile reverse osmosis system available today. All internal mechanical systems are mounted on a strong lightweight aluminum frame enclosed in a ruggedized military style case. The 2000DM utilizes water sources ranging from fresh surface or well water to heavy sea (salt) water.  This versatility comes from a unique pumping and injection system, with a variable recovery rate, producing the maximum product flow from the feed water. 
  • The ASPEN 10,000CM water purification system will supply 8,500 to 10,000 gallons per day (between 300 and 400 gallons per hour) of highly purified water from virtually any non-saline water source. Water can be drawn from ditches, ponds, rivers, lakes or standing water that may contain chemical and biological contamination.
  • The ASPEN 1800 Brief Case and/or Backpack water purification systems will supply up to 1,800 gallons per day (75 gallons per hour) of highly purified water from virtually any non-saline water source. Water can be drawn from ditches, ponds, rivers, lakes or standing water that may contain chemical and biological contamination.

NORIT / PENTAIR


Pentair, Inc. recently acquired Clean Process Technologies (CPT), a division of privately held Norit Holding B.V. As of May 12, the companies under CPT – Filtrix, Haffmans, Nijhuis, Norit Components & Services, Norit Process Technology, Südmo, and X-Flow – are part of Pentair’s Filtration Solutions global business unit.


Pentair Clean Process Technologies provide greater process efficiency, longer life cycles, and cost savings ensuring a more sustainable operation. Our membranes, pumps, aseptic and hygienic valves, carbon dioxide systems, and quality control equipment rank among the world's best. We offer global coverage with research and development, engineering, and manufacturing facilities in seven countries. As part of Pentair's Filtration Solutions global business unit, the CPT companies, together with a network of dedicated sales and service centers, business partners, and distributors, serve customers in more than 150 countries around the world.